Fire-Suit & Accessories
Signature Aluminium Coat
DSZALC.2L–5L · closed body coat · free size, per piece
₹6,400.00/ NOS
Signature aluminium coat · Howrah foundry belt
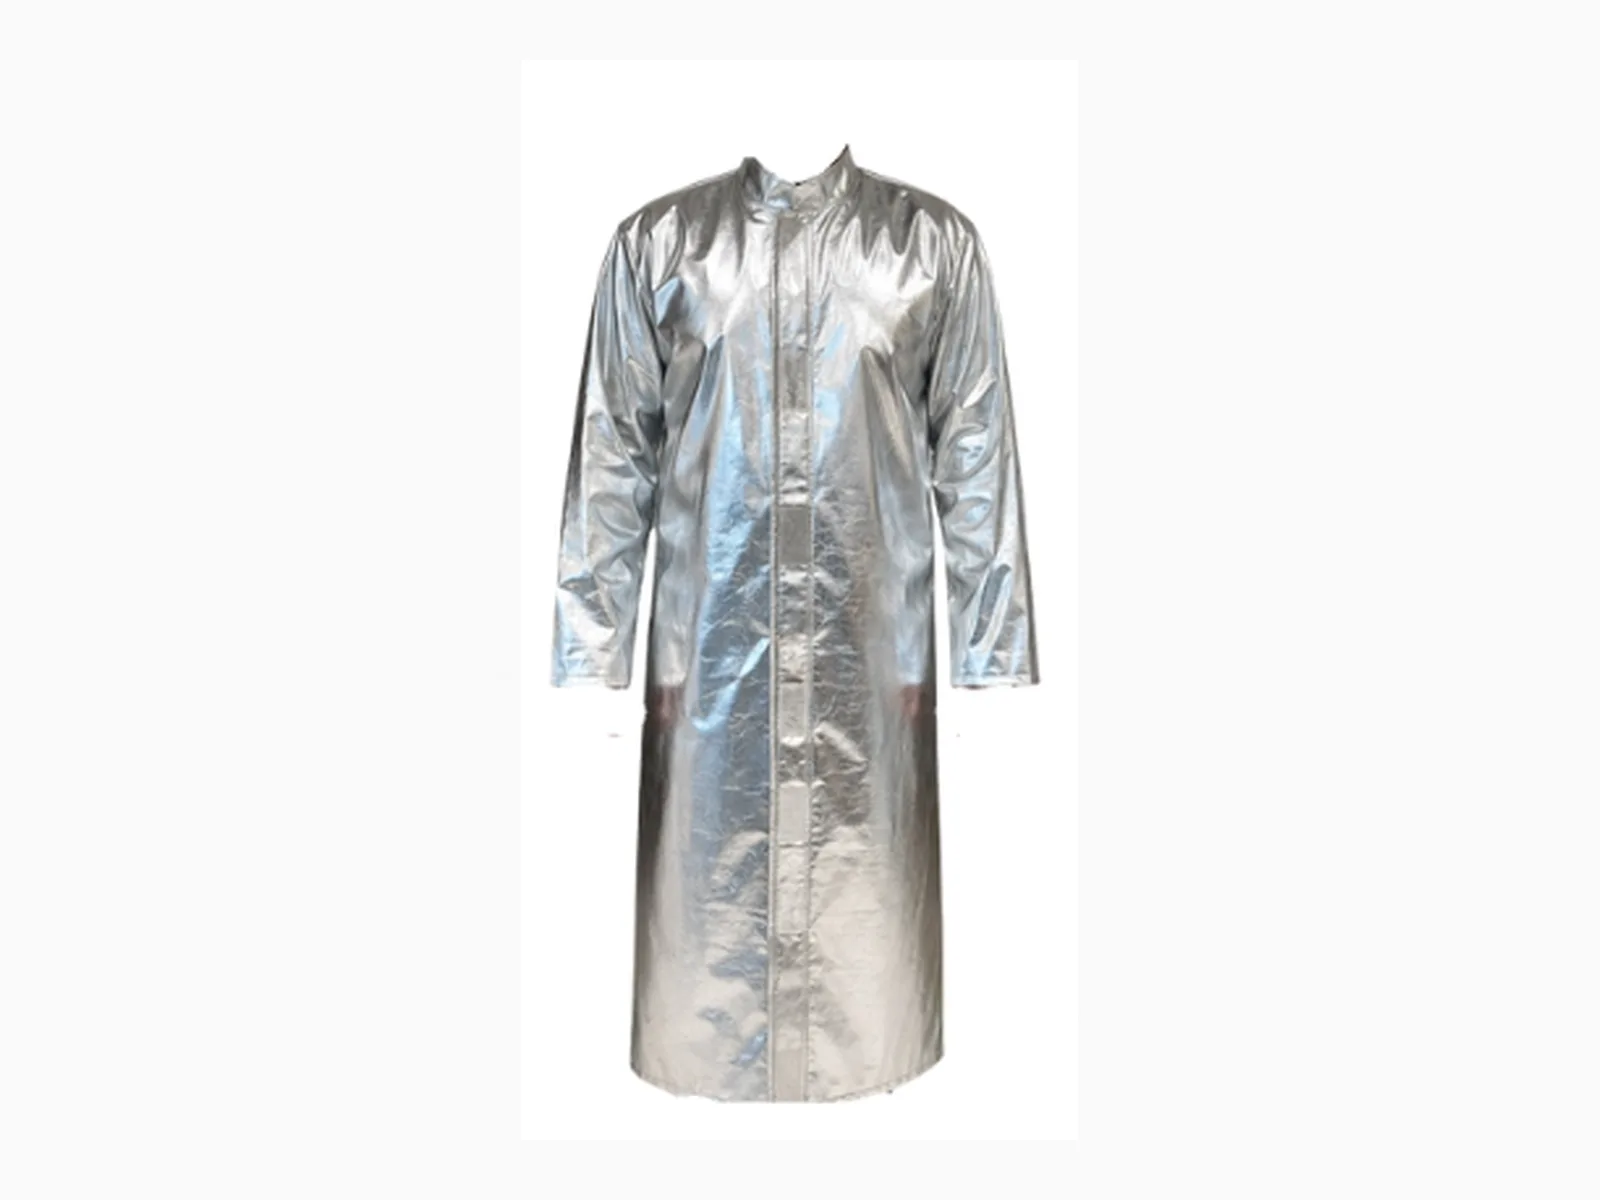
When a cupola is tapped or a ladle is carried down the pouring line, radiant heat hits the whole body, not just the hands. The Signature Aluminium Coat is the closed body layer of an aluminized kit, with a silver aluminium-coated face, free size, in four builds from DSZALC.2L to DSZALC.5L. Below you will find which build suits which foundry job, how the coat works with gloves, an apron or a proximity suit, and how to put a crew-wide order together. Coats are made in Ahmedabad and dispatched to Kolkata and Howrah.
Fire-Suit & Accessories
DSZALC.2L–5L · closed body coat · free size, per piece
₹6,400.00/ NOS
The coat leaves the hands uncovered, and bench crews often need only front cover. Quote gloves and aprons on the same request as the coats.
On a melt floor, three jobs put the body in front of radiant heat: tapping, pouring and tending the furnace. Each one exposes the body differently, so each job gets its own starting build.
Cupola spout or induction furnace lip
The tapper holds position facing the molten stream while the ladle fills. Chest, arms and thighs take the heat for the whole tap, and the body cannot step back until the ladle is full.
Starting build: DSZALC.4L or DSZALC.5L
Moulding floor and pouring line
Pourers carry or steer a full ladle along a row of moulds. The heat moves with them, so they need cover on the sides and arms as well as the front, and they walk a lot between moulds.
Starting build: DSZALC.2L or DSZALC.3L
Charging doors, de-slagging and sampling
Charging, raking slag and taking samples mean short spells at an open furnace, repeated through the shift. Pick the build by how long each spell lasts on your floor.
Starting build: DSZALC.3L or DSZALC.4L
West Bengal's foundry trade is concentrated in Howrah, on the west bank of the Hooghly. Coke-burning cupolas do most of the iron melting, with induction furnaces in some units. These are typical starting points for each area; your own jobs decide the final mix.
Long-established foundry and re-rolling area, north Howrah
Grey-iron casting from cupolas, with re-rolling mills nearby running reheating furnaces.
Coat plan: Heavier builds for spout crews; lighter builds for re-rolling hands
Foundry locality on the north side of Howrah town
Daily cupola heats feeding hand-poured moulds on compact floors.
Coat plan: DSZALC.2L or DSZALC.3L for ladle crews who move between moulds
Foundries mixed with engineering workshops
Melting next to machining and fabrication, plus casting clean-up at the bench.
Coat plan: Coats for melt and pour crews; aprons for bench-side finishing
Foundry pockets within the wider Howrah cluster
Repeat casting runs where the same crews charge, tap and pour every heat.
Coat plan: A mixed order, one build per job, so every role is covered
Purpose-built foundry park in Howrah district
Newer and expanding melt shops that often kit out a whole crew at once.
Coat plan: Full first issue: coats, glove pairs and aprons quoted together
Industrial park developed by WBIIDC in Howrah district
Iron and steel casting alongside engineering, with furnace-side maintenance work.
Coat plan: DSZALC.3L as a general issue, adjusted per job
The coat is one part of an aluminized kit. Each Signature piece covers a different part of the body and carries its own listed figure, and a figure on one piece never carries over to another.
| Part | Product and models | Covers | Listed working temperature | Order |
|---|---|---|---|---|
| Body | Signature Aluminium CoatDSZALC.2L to DSZALC.5L | Torso, arms and back in a closed, free-size coat | 700 °C to 900 °C | |
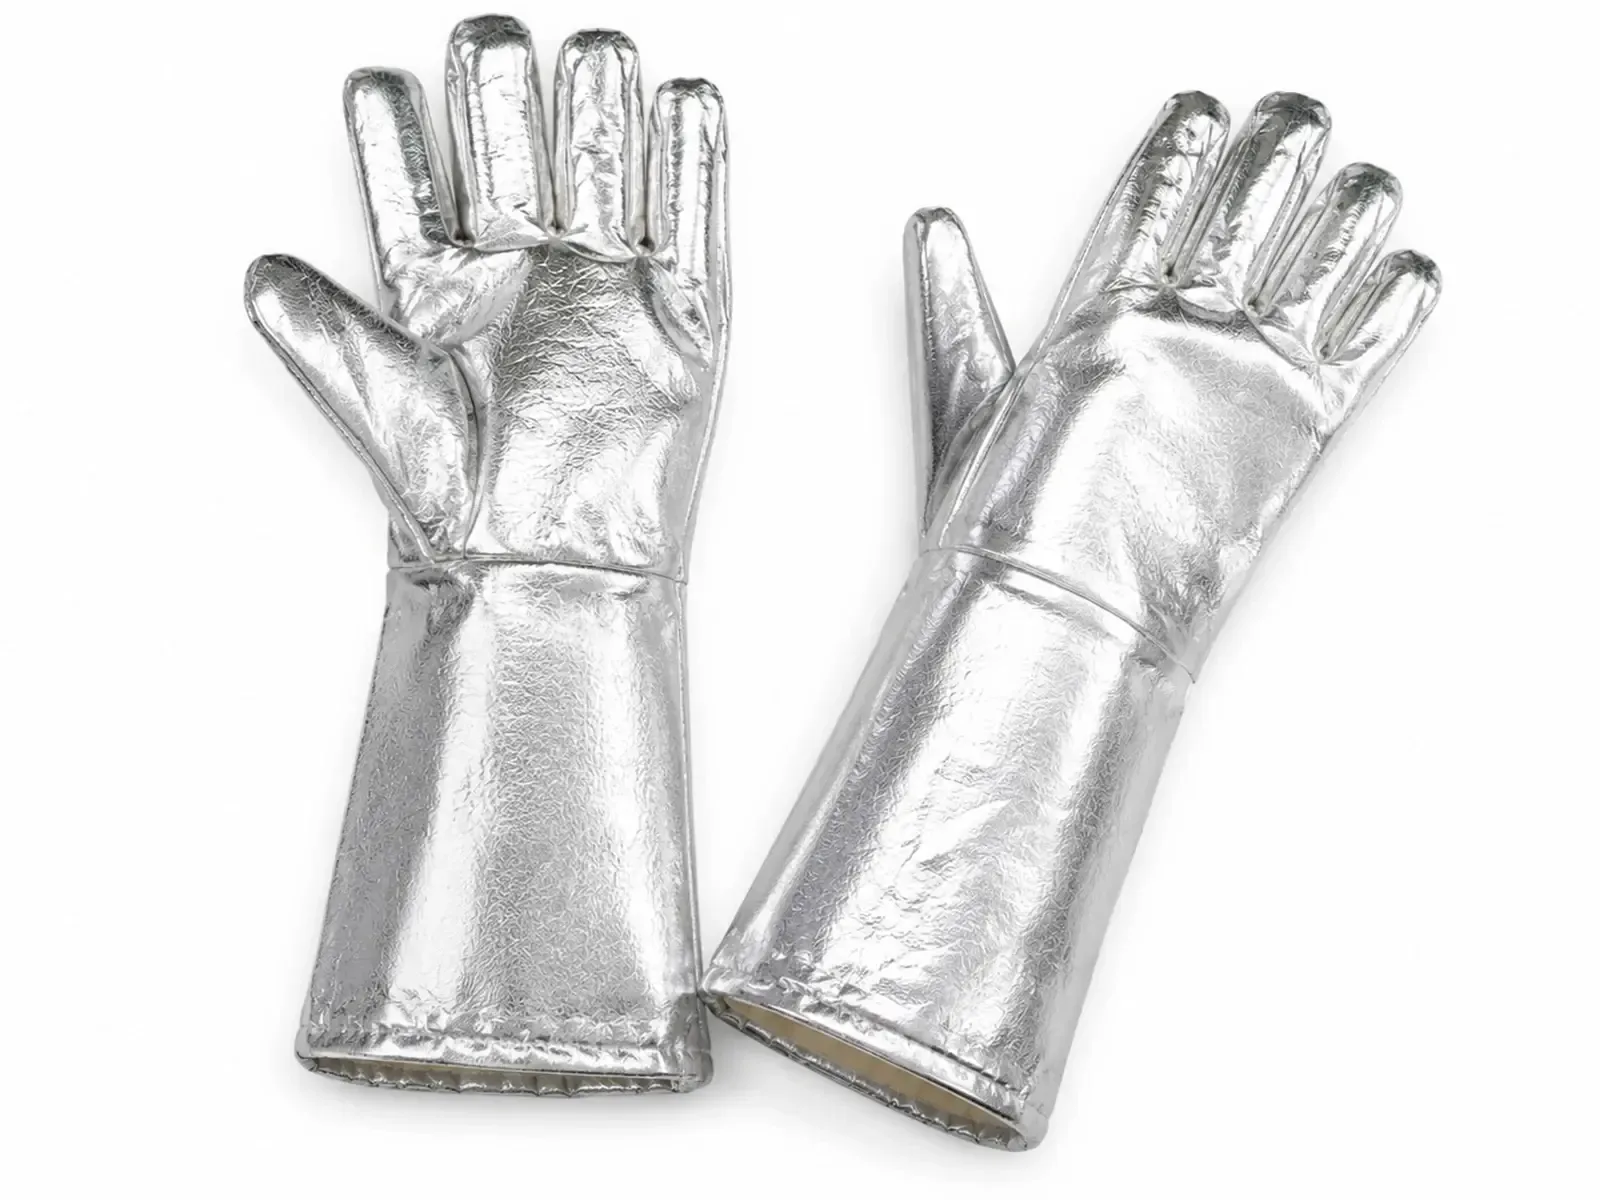
| Hands | Signature Aluminum GlovesDSZALHG, per pair | Hands, wrist and lower forearm, 14 inch, 2 layer | Not listed | |
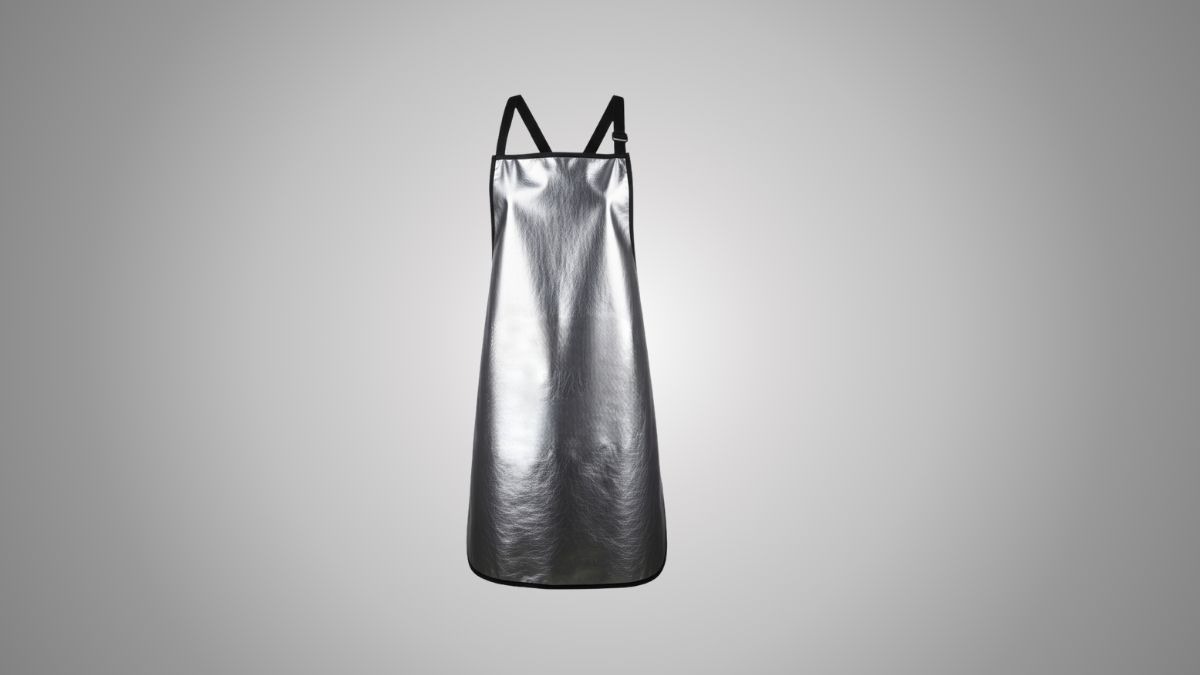
| Front only | Signature Aluminized ApronDSZALAP2.0 to DSZALAP5.0 | Front of the body, 24 × 36 inch, for one-direction heat at the bench | 600 °C to 800 °C | |
| Full suit | Signature Fire Proximity SuitDSZAL.2LS to DSZAL.5LS | Free-size suit for sustained close work near intense heat | 600 °C to 1000 °C |
The listed temperature is the same on every build, so the choice comes down to how long a person stays in front of the heat and how much they walk. To compare figures from different suppliers, see our guide to reading temperature ratings.
| Build | Layers | Approx. weight | Suits |
|---|---|---|---|
| DSZALC.2L | 2 layers | About 5 kg | Pourers and helpers who walk the moulding floor all shift |
| DSZALC.3L | 3 layers | About 6 kg | Furnace tenders and mixed roles that switch between jobs |
| DSZALC.4L | 4 layers | About 7 kg | Tappers and crews working at open furnace doors |
| DSZALC.5L | 5 layers | About 8 kg | The longest spells facing a tap or an open melt |
This closed DSZALC coat is a separate product from the Signature Back Open Coat, which leaves the back open for ventilation and is listed at 600 °C to 800 °C. No product standard such as EN 469 is listed for the DSZALC coat. Darshan Safety Zone is ISO 9001:2015 certified as a company.
The reflective face is the part that matters. Once it is cracked or worn through, the coat protects less than it seems to.
Step 1
Fit check on day one
Put the coat on each wearer over their usual work clothes and check the cuffs, hem and closure for gaps.
Step 2
Look before every heat
Scan the silver face and the seams before charging, tapping or pouring starts.
Step 3
Pull damaged coats
A coat with cracked, peeled or worn-through coating comes out of service, even if the rest looks sound.
Step 4
Hang it dry
Between shifts and through the monsoon, hang coats or lay them flat in a dry place, with no hard folds.
Coats are issued per person and sized as free size, so a crew order comes down to jobs, head count and builds. Work through these five steps and send them in one request.
1
List the hot jobs
Tapping, pouring, furnace tending, de-slagging or anything else that puts people in front of the heat.
2
Count heads per shift
The number of people on each job across every shift, so nobody shares a coat between shifts.
3
Pick a build per job
One DSZALC model for each job, using the build table above, each on its own line.
4
Add spares and the rest of the kit
Spare coats, DSZALHG glove pairs, and aprons or proximity suits where your procedure calls for them.
5
Send the address and date
The Kolkata or Howrah delivery pin and the date you need the kit on site.
There is no Darshan Safety Zone branch, dealer or warehouse in West Bengal. Coats and the rest of the aluminized kit ship from our Ahmedabad factory to the foundry or stores address on the order, and dispatch timing is confirmed on each quotation.
Some jobs keep a person close to intense heat for a sustained stretch. If your procedure calls for a full suit, quote the Signature Fire Proximity Suit (DSZAL.2LS to DSZAL.5LS, free size, about 6 to 10 kg, listed at 600 °C to 1000 °C) for those people and keep coats for the rest of the crew.
Plan the wider foundry programme, browse every aluminized piece, or get help with a mixed order.
How aluminized PPE sits within a full foundry heat and hot-work programme.
Open industry journeyThe full Signature aluminized range: coats, aprons, gloves and proximity suits.
Browse the categoryWhat to put in a multi-line PPE request so the quote comes back complete.
Read the guideUnsure whether a job needs a coat, an apron or a full suit? Describe it and we will reply.
Open contact formQuestions Kolkata and Howrah foundry teams ask about the aluminium coat.
It is body PPE. The closed coat covers the torso, arms and back with a silver aluminium-coated face that reflects radiant heat from a cupola spout, a full ladle or an open furnace. It does not cover the hands, so the crew still needs aluminized gloves, and it is not a full proximity suit.
All four builds are listed at 700 °C to 900 °C, so pick by how long the wearer faces the heat and how much they move. Pourers walking a ladle along the moulds often prefer DSZALC.2L (about 5 kg) or DSZALC.3L (about 6 kg). Tappers who hold position at the spout, and furnace tenders working at an open door, usually go to DSZALC.4L (about 7 kg) or DSZALC.5L (about 8 kg). Confirm each choice against the foundry's own PPE rules.
No. The only temperature listed for the coat is a working temperature of 700 °C to 900 °C, the same on all four builds, and no product standard such as EN 469 is listed for it. Darshan Safety Zone holds ISO 9001:2015 as a company. If your purchase procedure asks for particular documents, mention them in the enquiry and we will tell you what we can provide.
Yes. The coat stops at the cuffs. Add Signature Aluminum Gloves DSZALHG, a 2-layer aluminum-coated glove 14 inch long and sold per pair, so the hands holding tongs and ladle handles are covered too. No working temperature is listed for the gloves, so the coat's figure should not be read across to them.
The Signature Aluminized Apron (DSZALAP2.0 to DSZALAP5.0, 24 × 36 inch, listed at 600 °C to 800 °C) covers only the front. It suits knock-out, fettling and bench work where the heat comes from one direction. When heat reaches the arms, sides and back, as it does beside a tapping spout or under a ladle, the closed coat is the better choice.
The Signature Fire Proximity Suit (DSZAL.2LS to DSZAL.5LS, free size, listed at 600 °C to 1000 °C) is a full suit for sustained close work near intense heat. The coat is for routine foundry duty where a coat and gloves, with an apron where needed, are enough. Let your site procedure decide which jobs move up to a suit.
Every DSZALC build is free size and cut to go over work clothing. Put the coat on each wearer before the first shift and check the cuffs, hem and closure. Gaps let heat reach the body. The four listed builds are what we quote; ask before ordering if your programme needs something different.
List the jobs that put people in front of the heat, such as tapping, pouring and furnace tending. Count the people on each job per shift and choose a DSZALC build for each job. Add spare coats, then glove pairs and any aprons. Send it all as one quotation request with separate lines and the delivery pin.
Keep coats dry between shifts, hung or laid flat, and never folded tightly, because a hard crease can crack the reflective face. Check the aluminium face and the seams before every use. Take a coat out of service once the coating is cracked, peeled or worn through.
Signature aluminized PPE is made by Darshan Safety Zone in Ahmedabad, Gujarat. There is no branch, dealer or warehouse in West Bengal; orders are dispatched from Ahmedabad to the Kolkata or Howrah address on the order. Dispatch timing depends on models and quantities and is confirmed on the quotation.
Send the hot jobs, people per shift, the DSZALC build for each job, any gloves or aprons, and the delivery pin. We will come back with one quotation for the whole kit.